
AI Decision Engine
For decision inputs, constraints, and recommendations.
ExploreAutomotive production depends on coordinated equipment, stable material flow, quality requirements, and changing build schedules. Operational optimization connects production conditions with decisions that help teams manage throughput, resource use, and response time. When a decision leads to physical action, the workflow also needs clear authorization, defined operating limits, and confirmation that the equipment reached the intended state.
An assembly line can lose time when a station falls behind, a tool becomes unavailable, a component is delayed, or a quality check requires additional review. Optimization can help production engineers and operations leaders assess these conditions together rather than treating each event in isolation. The objective may be to reduce waiting, balance station workloads, manage energy use, or prioritize a response while preserving cycle-time targets, quality rules, worker safety, and equipment limits.
A useful design begins with a defined production problem. For example, a team may examine how body-shop station status, equipment availability, work-in-progress, and the approved build schedule affect the next production decision. The selected approach should be compared with the plant’s current method using the same demand and operating assumptions.
Optimization depends on timely, well-contextualized information. Relevant inputs may include production orders, station cycle times, equipment state, sensor readings, quality holds, material availability, and maintenance status. Each record should be associated with the correct asset or station and include usable timestamps and data-quality indicators. Missing, delayed, or conflicting observations should be identified before they influence a decision.
Artificial intelligence (AI) and rule-based logic can support different parts of the workflow. Rules may enforce fixed production constraints, while analytics can help identify bottlenecks, compare possible schedules, or rank response options. The method should expose its objective, constraints, input assumptions, and uncertainty so manufacturing engineers can evaluate whether a recommendation fits the actual line.
Not every optimization result should directly control equipment. Implementations can begin with recommendations for a production supervisor, progress to commands that require human approval, or consider bounded autonomous execution only after the equipment interface and operating conditions have been validated. The appropriate mode depends on the action, its consequences, the quality of available state information, and the plant’s existing controls.
For a defined use case, the action path should identify the target equipment, command interface, permission checks, operating limits, and expected response. A request to create a maintenance work order is different from a command that changes equipment behavior. Existing machine protections and safety functions must remain independent of an AI recommendation and must not be bypassed by the optimization workflow.
A command acknowledgment alone does not prove that the physical operation completed as intended. The workflow should compare the requested action with subsequent evidence, such as a sensor reading, controller state, station status, or independently observed equipment position. It should record rejected commands, timeouts, partial execution, communication loss, operator overrides, and recovery steps.
Where observations are stale, constraints are violated, or the system encounters a condition outside its evaluated range, the workflow should stop, abstain, or escalate according to the approved design. The exact fallback behavior must be selected with the plant’s engineering and controls teams and tested before operational use.
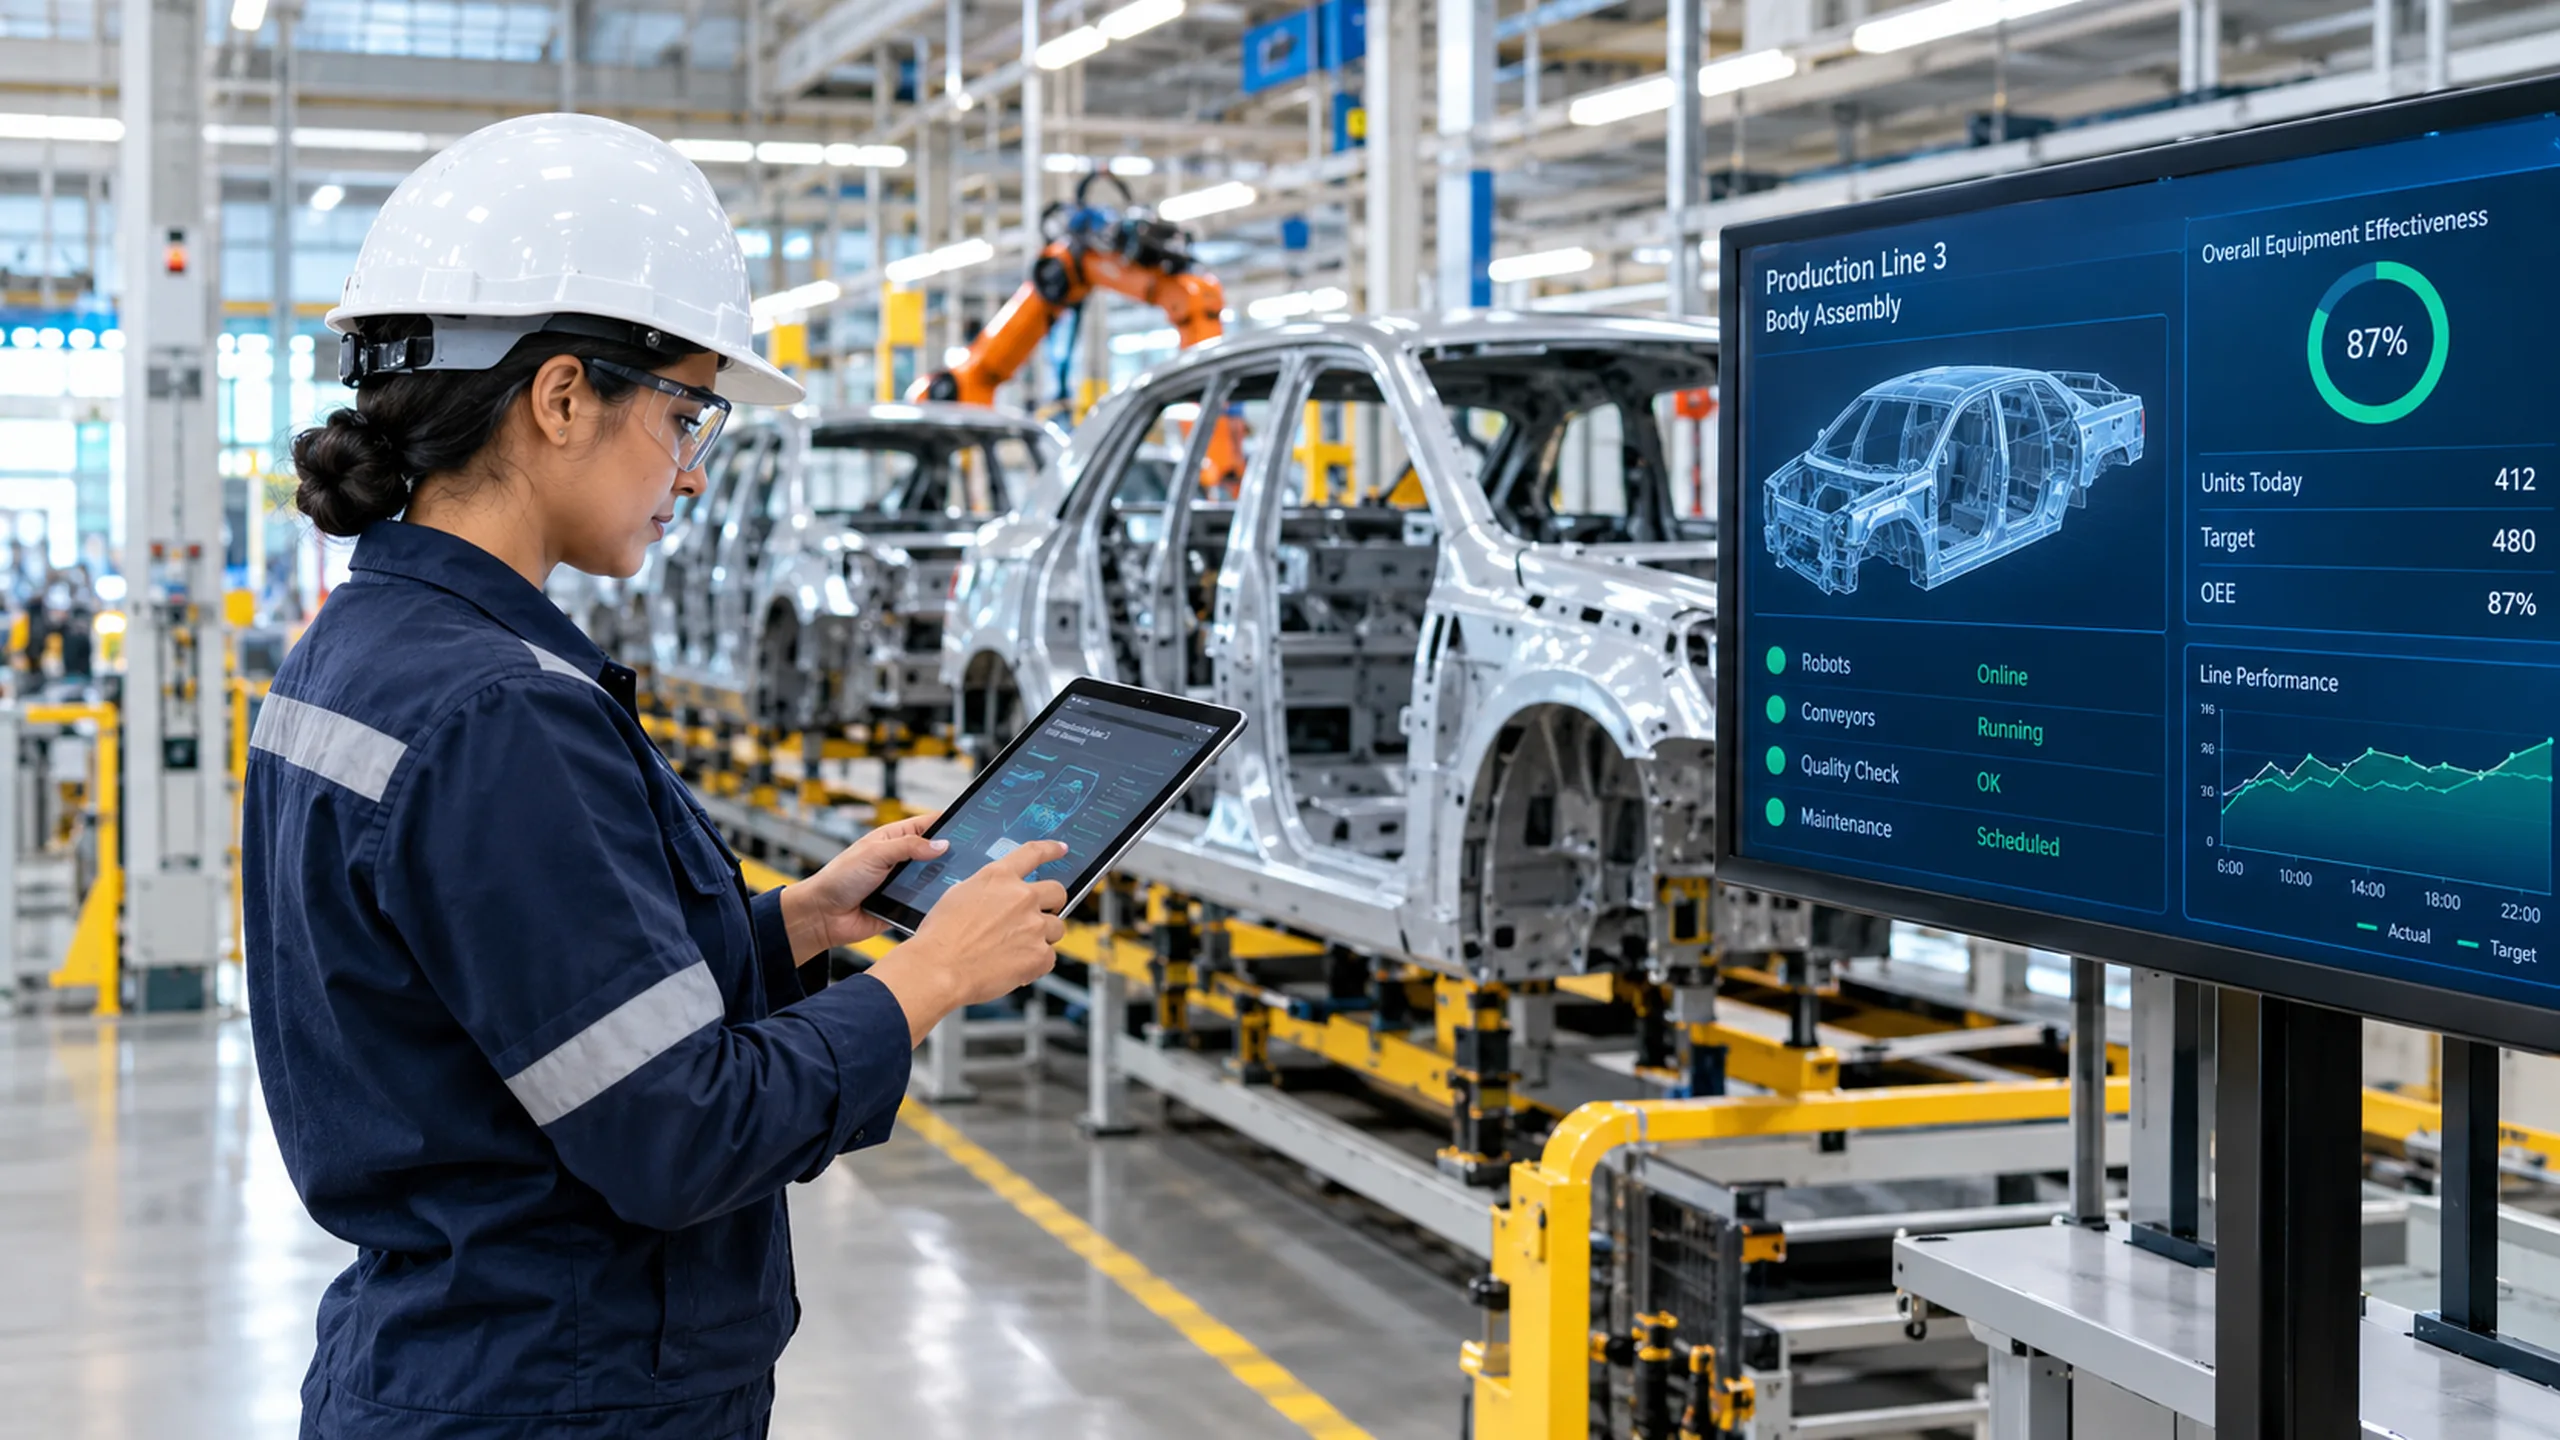
A pilot should define its baseline policy, production objective, operating constraints, and acceptance criteria before comparing approaches. Depending on the use case, measures may include throughput, cycle-time variation, queue or waiting time, resource utilization, energy consumption, quality holds, and response time. Action-related measures should include constraint violations, rejected or timed-out commands, operator interventions, successful completion checks, and recovery behavior.
Separate analytical performance from operational benefit. A simulated improvement is not evidence of a production result, and an earlier alert does not establish avoided downtime unless the analysis accounts for feasible intervention, available resources, and the effect of that intervention. Any simulation-based case study should clearly identify synthetic data, assumptions, evaluation methods, and limitations. A customer pilot should then test the approach with authorized site data and representative operating conditions.
Implementation planning should identify the source of each data field, the systems that own production records, and the boundary between analytics and machine control. Depending on the facility, relevant interfaces may include manufacturing execution, enterprise resource planning, maintenance systems, industrial controllers, gateways, and edge or server-based applications. Compatibility should be confirmed for the specific devices, protocols, software versions, and access policies involved rather than assumed from a general technology label.
A practical assessment covers data availability, time synchronization, latency, network interruptions, access control, logging, change management, commissioning, and responsibility for ongoing support. The result should be a clearly scoped workflow with named owners, measurable acceptance criteria, and an agreed plan for handling conditions that the system cannot safely or reliably resolve.
Operational optimization connects with several related areas:
For decision inputs, constraints, and recommendations.
ExploreFor the action path and outcome feedback.
ExploreFor equipment interfaces, permissions, and control boundaries.
ExploreFor evaluation questions around constrained decisions and verified outcomes.
ExploreStart with one production bottleneck, equipment adjustment, or bounded response that can be evaluated against a documented baseline. Bring the relevant process owner, manufacturing engineer, controls specialist, and IT or OT representative into the discussion. Together, define the available data, decision authority, operating limits, integration requirements, and evidence needed to judge the result.