
AI Software and Analytics for OEM Vehicle Manufacturing
AI software can help OEM vehicle manufacturers interpret production data, identify unusual operating patterns, assess visual quality, and support planning decisions. Its value depends on the quality and coverage of the available data, the conditions under which models are evaluated, and how results enter existing production and quality workflows.
Contact OEMNex
Introduction
This page covers the software implementation behind AI-supported analysis. It complements the AI Decision Engine, which describes the decision functions, while this page focuses on data preparation, model execution, deployment, and ongoing evaluation.
Preparing Production Data for Analysis
Production data may come from manufacturing execution systems, quality records, machine and process sensors, inspection images, maintenance histories, and production planning systems. Before analysis, each dataset needs a defined purpose, reliable timestamps, consistent units, meaningful asset or process identifiers, and documented data-quality rules.
Training and evaluation records should represent the range of vehicle models, components, production shifts, equipment states, lighting conditions, and process variation relevant to the intended task. Quality labels need clear definitions and review procedures. Missing records, duplicate events, sensor drift, inconsistent labels, and changes in inspection practice can distort model results if they are not identified.
Keep dataset lineage and version information so reviewers can trace which source records, transformations, labels, and feature-generation steps were used. Separate development data from evaluation data, and prevent information from the future or target outcome from leaking into model inputs. Evaluation should use representative conditions that were not used to fit or tune the model.
AI Methods for Production and Quality Workflows
Different manufacturing tasks require different methods. Anomaly detection can flag patterns that differ from an established operating baseline. Prediction can estimate a defined future measure when suitable historical examples exist. Computer vision can assess visible characteristics such as surface finish, component presence, fit, or assembly features, provided image quality and labeled examples support the task. Optimization methods can compare production choices against explicit objectives and constraints.
Method selection should start with the operational question rather than the algorithm. Define the input data, expected output, acceptable uncertainty, baseline method, and how a person or downstream system will use the result. For example, a paint-finish inspection model should be evaluated against reviewed defect labels across relevant colors, surfaces, lighting conditions, and line speeds. A model alert is an assessment for review, not proof that a defect exists or that a production line should automatically stop.
Using Analytics in the Production Environment
AI models may run on an edge computer near the production process or on a server, depending on response time, data volume, connectivity, computing resources, security requirements, and maintenance arrangements. The deployment choice should be confirmed for the actual facility; no single arrangement is suitable for every plant.
Model outputs should be passed to defined interfaces such as a quality review queue, maintenance workflow, production report, or an approved enterprise application. Record the model version, input time, relevant asset or process identifier, result, confidence or uncertainty where available, and any human disposition. If a result can influence a physical action, the command path, authorization, independent protective functions, and outcome verification require separate engineering review.
Monitoring, Evaluation, and Model Maintenance
Performance can change when vehicle variants, suppliers, materials, equipment, process settings, camera placement, or environmental conditions change. Monitor data quality and the distribution of incoming observations, not just model output. Review false alerts, missed defects, uncertain cases, processing delays, and changes in workload with the production and quality teams.
Set responsibilities for reviewing performance, approving model updates, testing a new version, and restoring a previously approved version if a change causes problems. Retraining should follow an evidence-based process with representative data, controlled evaluation, documented approval, and version tracking. A detected change in data does not automatically mean retraining is appropriate.
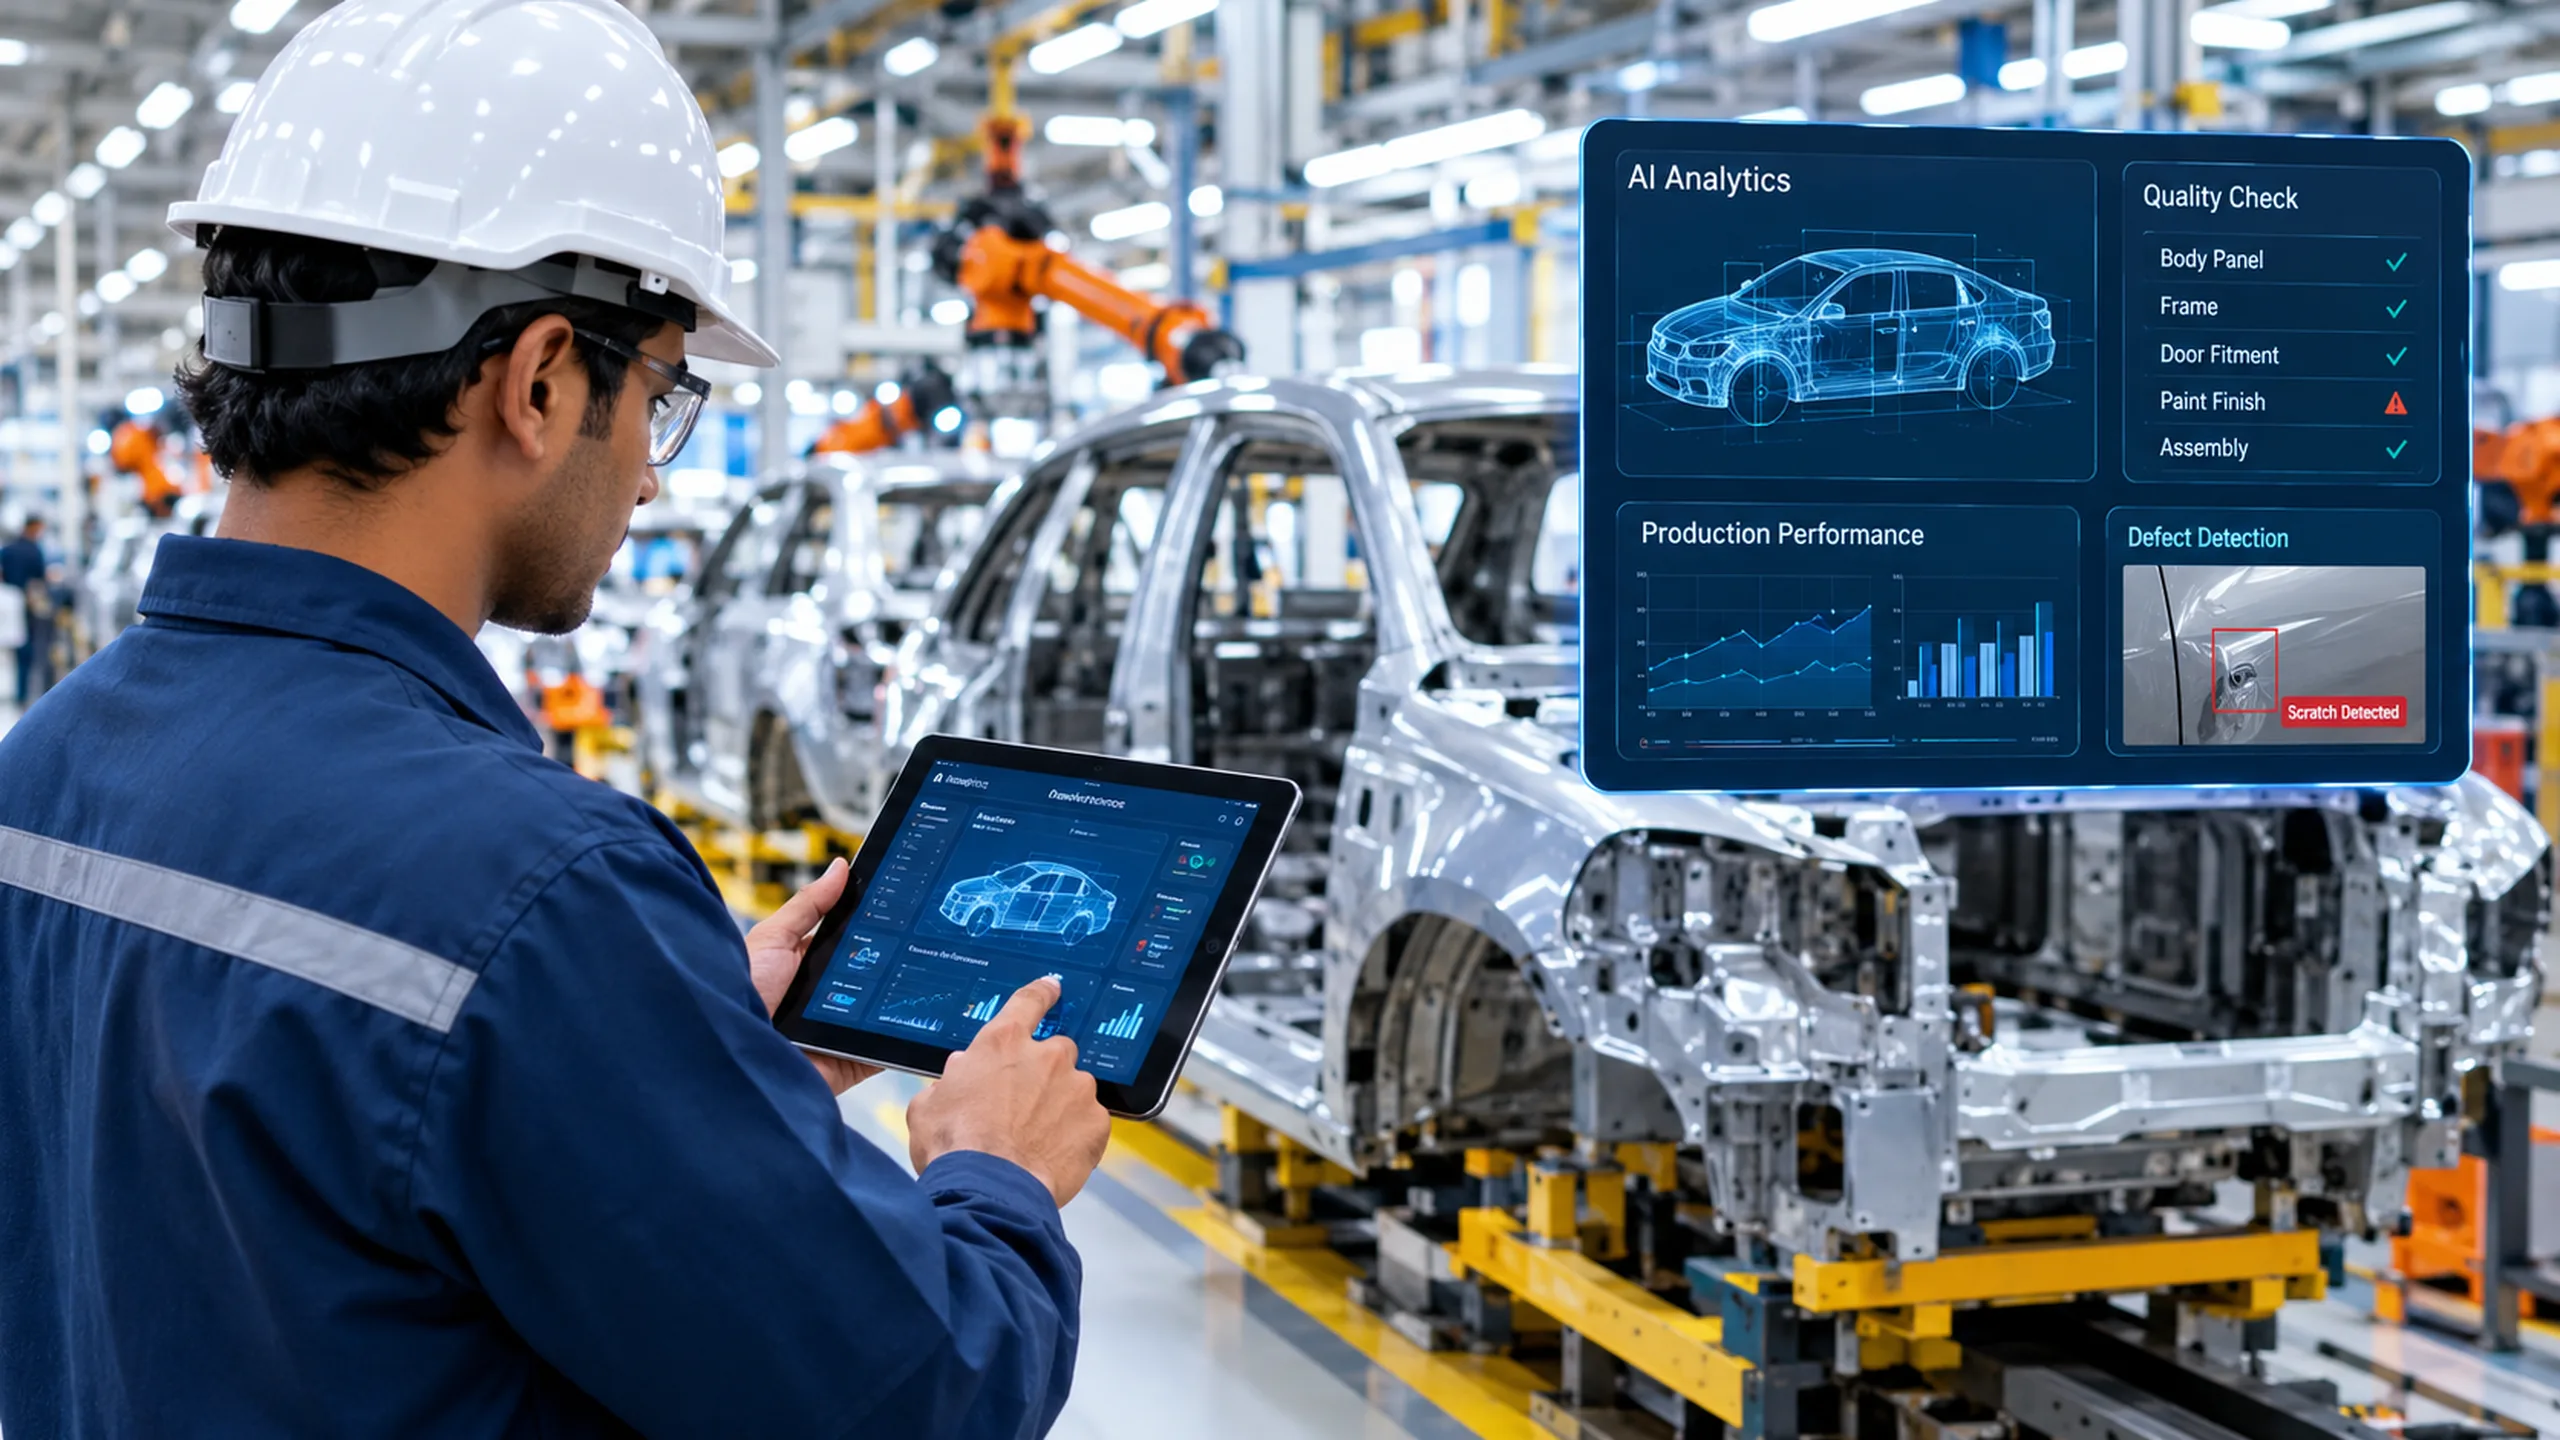
Use measures that match the task. Examples include defect recall and false-accept rate for inspection, false alerts per operating hour for anomaly detection, prediction error for forecasting, and processing latency for time-sensitive applications. Define each metric's unit, denominator, evaluation period, and exclusions. Compare results with a credible existing rule or workflow, and report limitations alongside the findings.
Implementation Evidence and Next Steps
Before production use, distinguish functions that have been tested from proposed designs and interfaces that still need validation. A software demonstration does not establish performance on a live production line, compatibility with every device, or readiness for automated control. Evaluation should use approved data, documented acceptance criteria, and the operating conditions expected at the facility.
A practical starting point is to select one bounded workflow, identify its data owner and operational reviewer, document the current baseline, and agree on evaluation criteria before testing a candidate method. The pilot should examine data completeness, model performance, integration effort, user response, failure handling, and the evidence needed before any wider deployment.
To discuss a suitable evaluation approach, contact the OEMNex team through the contact page.